Wednesday, April 22, 2015

TREE - COUROUPITA GUIANENSIS or CANON BALL or KAILASPATI


COUROUPITA GUIANENSIS or CANON BALL or KAILASPATI 
Post 121 - by Gautam Shah 


These trees are as amazing, as their name “Canon ball” is. Its fruits are like large brown balls held on short twigs, and so appear to grow out of the trunk. Fruits take 8-9 months to ripen, fall and burst open with a loud crack. The flowers are large (up to 60 mm) with six petals, brightly coloured from pink to crimson coloured near the base, and yellowish toward the tips. Flowers have sweet smell at night and in the early morning. The ripe and bust fruit balls give a foul stench, which attracts bees and animals.

Cannon Ball fruits
The tree, bark, leaves and flowers are used to treat hypertension, tumours, pain, inflammation, common cold, stomachache, skin conditions and wounds, malaria, and toothache, etc.


Young tree with fresh leaves April India
These are tall (35 to 50 mts) and erect deciduous trees. The leaves are long like a mango tree. They grow in clusters at the ends of branches. The leaves ripen to reddish colour, shed three times a year. The trees, however, do not remain bare for more than few days, as immediately new leaves appear giving a wonderful variegated green foliage. A tree can bear 1000 flowers per day.

Fresh leaves almost like Mango tree leaves
 The flowers’ bundle resembles “Shiva-lingam” a hooded snake or a Chhatra of Sheshnag. And for the same reason it is also called " Nag-lingam" or “Shiv-ful” (flower of Shiva). The tree is found in Shiv temple complexes and also Buddhists holy places across Asia.

Flowers of Cannon Ball or Kailaspati / Ling-ful

The tree is of Guinea origin, but is found in many parts of the world. Its popular name is Cannon ball tree. Its botanical name is Coroupita guianensis. In India it is known for 3000 years and known by Kailaspati, Shiv-fal, Shiv-lingi, Nag-lingam, etc. 


.

Friday, April 10, 2015

METALWORKING

Post 120 - by Gautam Shah
. 


Metals are very important materials, because these can be easily deformed into useful shapes, and several times over and over again. The shape, function, and appearance of metal objects are largely determined by the type of metal used. Metals as pure material and as alloys or in mixed states offer innumerable variation of properties. Metals show a wide range of unique characteristics when ‘worked’ over. These ‘working over the metal’ are related to temperatures and stress inductions. Metals also show varied behaviour under different use conditions.
Rusting is an indication How a metal is stressed
Metals begin to change during the conversion processes like casting, forging or rolling. Casting is a melt process but its environment, and cooling-period affect the quality of material. Forging and Rolling, are hot as well as cold processes, which stress the metal and cause alteration in its constituents and their arrangements. In cold working some temperature rise is inevitable. In hot conversion processes the reheating conditions, in-line scale removal, temperature maintenance, and cooling rate, all determine the quality of the product.

Welding heat can cause stresses in metals

There are several processes where unintentional heating of metal occurs. The heating conditions, local or total, include heavy stamping, shaping, forming, shearing, grinding, cutting, welding, and exposure to fire, change the quality of metal material. As these processes are unintentional, the effects cannot be foreseen, and realized in later part of the life of a metal. At such a late stage the section or component is not detachable and replaceable. Unintentional stresses are induced in existing structures when 1. one tries to cutout or attach a component, 2. allow consistent exposure of a structural member (like beam, truss, column, bracket) to fire (of kiln, stove, etc.), and 3. when rusted or damaged parts (such as in automobiles) are removed and replaced with fusion welding.

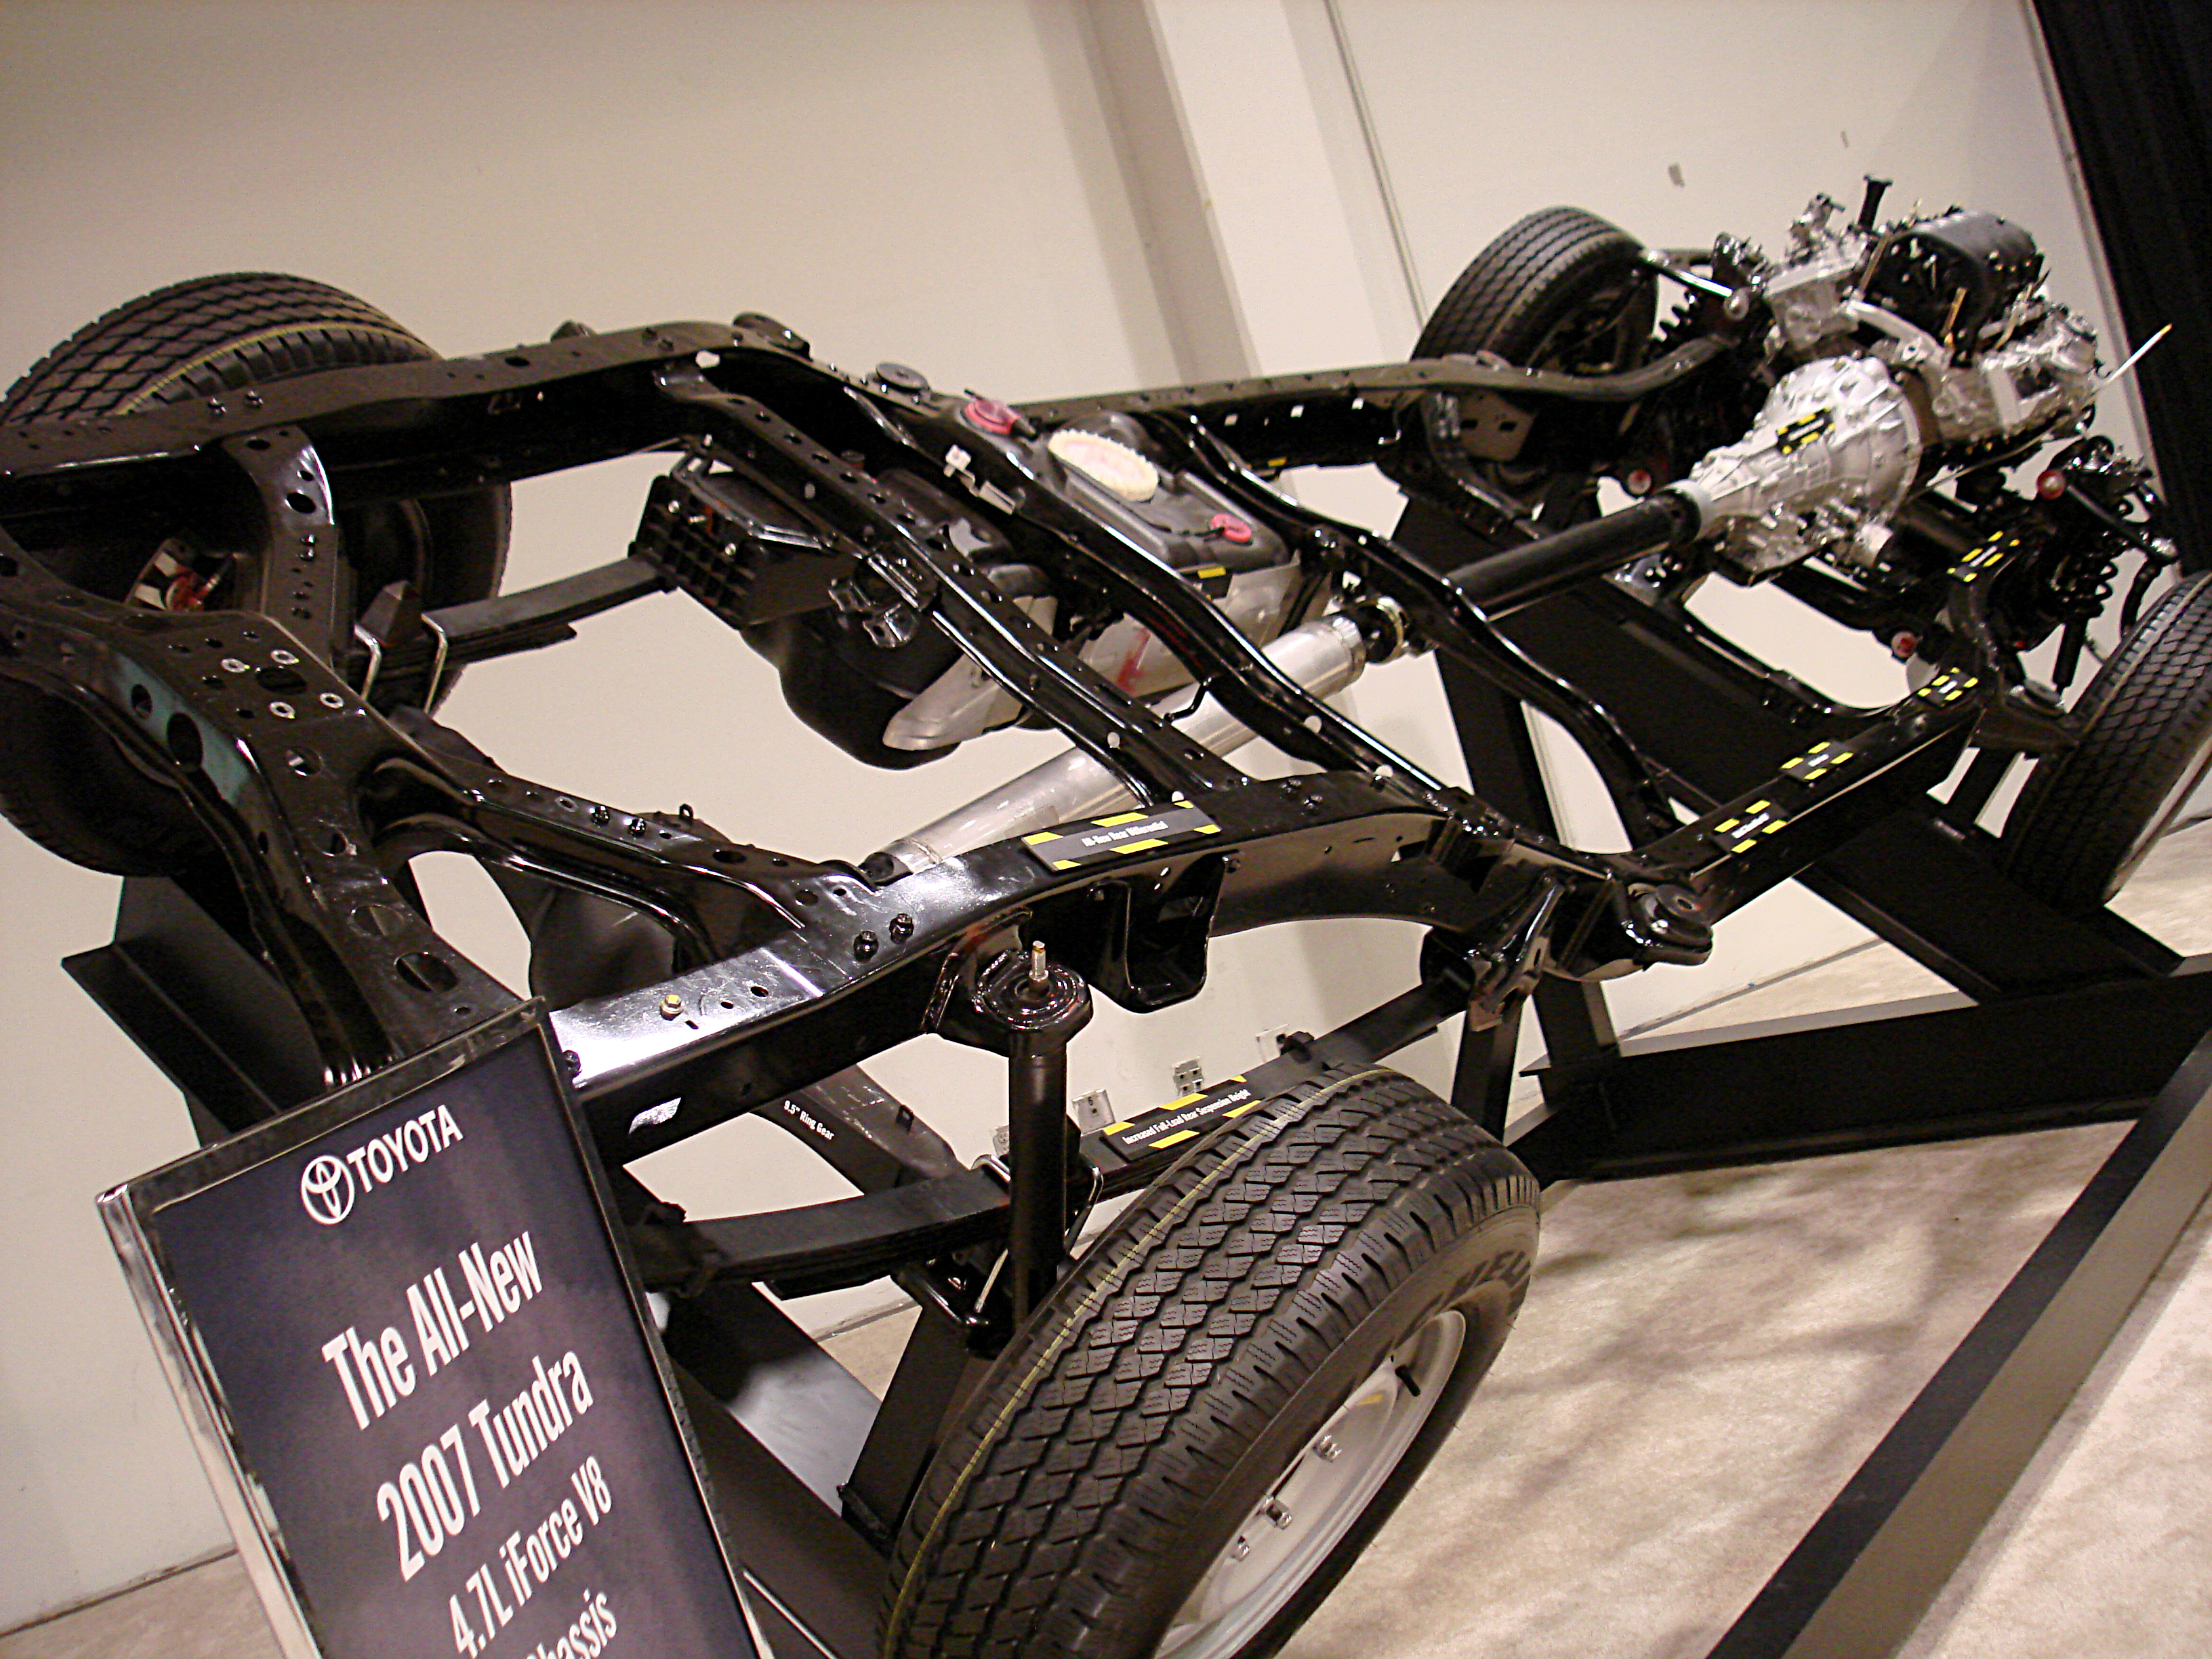
Toyota Tundra Chassis -is de stressed after assembly


Stresses in metal, existing (leftover of earlier processes) or newly set-in, affect the rate of corrosion, paint-ability, metal plating. Sometimes the final pass in hot-rolling generates specific surface patterns, for example, the protrusions on reinforcing bars or checkers on floor plates, ribs. In cold-rolling a specific surface roughness is rolled into strips at the temper mill to improve the deep-drawing operations and to assure a good surface finish on the final product.

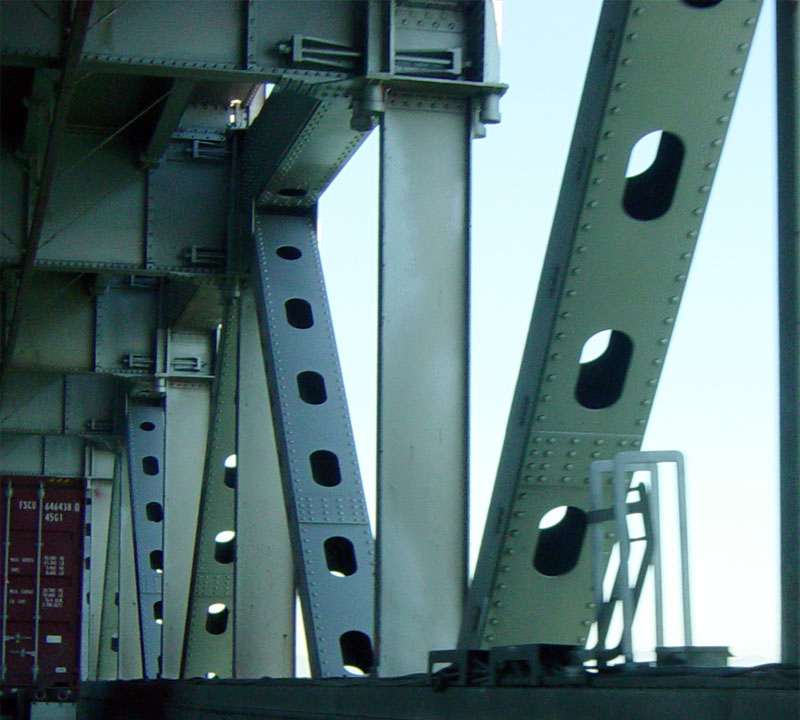
Retro-fitting of Oakland bridge
 

Hundreds of metalworking processes have been developed for specific purposes, but these can be divided into SIX broad groups: casting, rolling, extrusion, drawing, forging, and sheet-metal forming. The first five processes subject a metal to large amounts of strain. However, if deformations occur at a sufficiently high temperature, the metal will re-crystallize, that is, its deformed grains will be consumed by the growth of a set of new strain-free grains. For this reason, a metal is usually rolled, extruded, drawn, of forged above its re-crystallization temperature. This is called hot working, and under these conditions there is virtually no limit to the compressive plastic strain to which the metal can be subjected. Other processes are performed below the re-crystallization temperature. These are called cold working. Cold working hardens metal and makes the part stronger. However, there is a definite limit to the strain that can be put into a cold part before it cracks.
 

Scrape Containers
.

Wednesday, March 4, 2015

CLEAR COATINGS

CLEAR COATINGS

 Post 119 - by Gautam Shah
.


Clear coatings are primarily used to reveal the surface grain, colour and pattern, which however, are not always perfect or decent. Conditioning of the substrate surfaces is needed before application of a clear coating.
The most common problems with surfaces are like:
  • uneven colour
  • unsuitable tone
  • uneven grain or pattern
  • patchy absorbency
  • uneven texture
  • bleeding or soluble constituents
  • waxy or oily deposits
  • alkalinity
  • acidity
  • galvanic sensitivity
  • moisture content and transfer
Shellac toning over pine wood stripe

Such problems with man-made surfaces are controllable, at industrial production level, but with natural surfaces like the Wood, have to be tackled on the site. To overcome the surface related problems in clear coatings, many types of surface treatments are used. Most of the surface conditioners or treatments are fast drying, easy to apply, non destructive for the substrate and insoluble in the subsequent coat material. Surface conditioners are of following types: Fillers (transparent or opaque), levellers, sealers, stainers (soluble and insoluble colourants), printed patterns, patterning tools, etching agents, bleaches, and reactants.

Fillers - Sealers are used to fill in pores so that coating material does not sink into it, and provide an even finish. Fillers generally consist of an extender, a binder and occasionally a colourant. Extenders are fine grade powder of materials like gypsum, chalk, china clay, precipitated calcium carbonate, lime, asbestine, colloidal silica, barytes and talc. Binders could be water, gums, oils, alkyds and poly vinyl emulsions. Solvent bound fillers are better compared with water bound fillers which raise the grain or fibres of the surface. Colourants provide the necessary tint, to white extenders. Fillers, made of pigment powders, serve the purpose of filling as well as staining. Transparent fillers (low viscosity NC lacquer, shellac, etc.) are used to fill the pores and provide a sealing coat to the decayable material in the grains and vessels filled with gum exhudents.


Stains provide a correct transparent tint to the surface. Stains are generally dye-materials, soluble in water, oil or solvents. Water soluble stains though of many different varieties raise the fibres and are difficult to penetrate. Oil soluble stains are heavy bodied, take longer to dry out and interfere in the subsequent coating application. Solvent soluble stains are costly, dry out immediately and may bleed residual gums and other exhudents. Stains have one important drawback that they darken the existing colour of the substrate. Where timber surfaces need to be of lighter colour, surfaces have to be bleached or toned with opaque materials.
Clear coating on Leather
Bleaching process include a treatment with hydrogen peroxide followed by an alkaline accelerator like lime, caustic soda, sodium silicate or ammonia. Bleaching affects adhesion and toughness of coating, it also provides an amber hue to the coating on aging. 
Imposed patterns: On surfaces where there are very irregular grains, patterns are screen-printed, pressed or embossed using stains. Such patterns may emulate a wood grain pattern, or are just very fine mesh or lines. Staining is also done by micro spray guns, singeing, burning or carbon deposition from flames.


Post application treatments: Clear finishes often require some post application treatments. These are mainly burnishing and waxing. Burnishing is mainly done to NC lacquer, acrylic and melamine coatings to provide a glossy surface. Burnishing is not done to slow drying coatings, because such coatings, though are dry on outer face, take days to thoroughly dry out. Burnishing is done with a Carborundum like rubbing material with a waxy or oily base. Waxing provides a dull sheen and a protective coating. Waxing is also done to renovate old coatings. Waxing compounds also include a small amount of oils and sometime silicone materials.

.

Monday, February 23, 2015

FLOOR FINISH SYSTEMS -types


Post 118 -by Gautam Shah


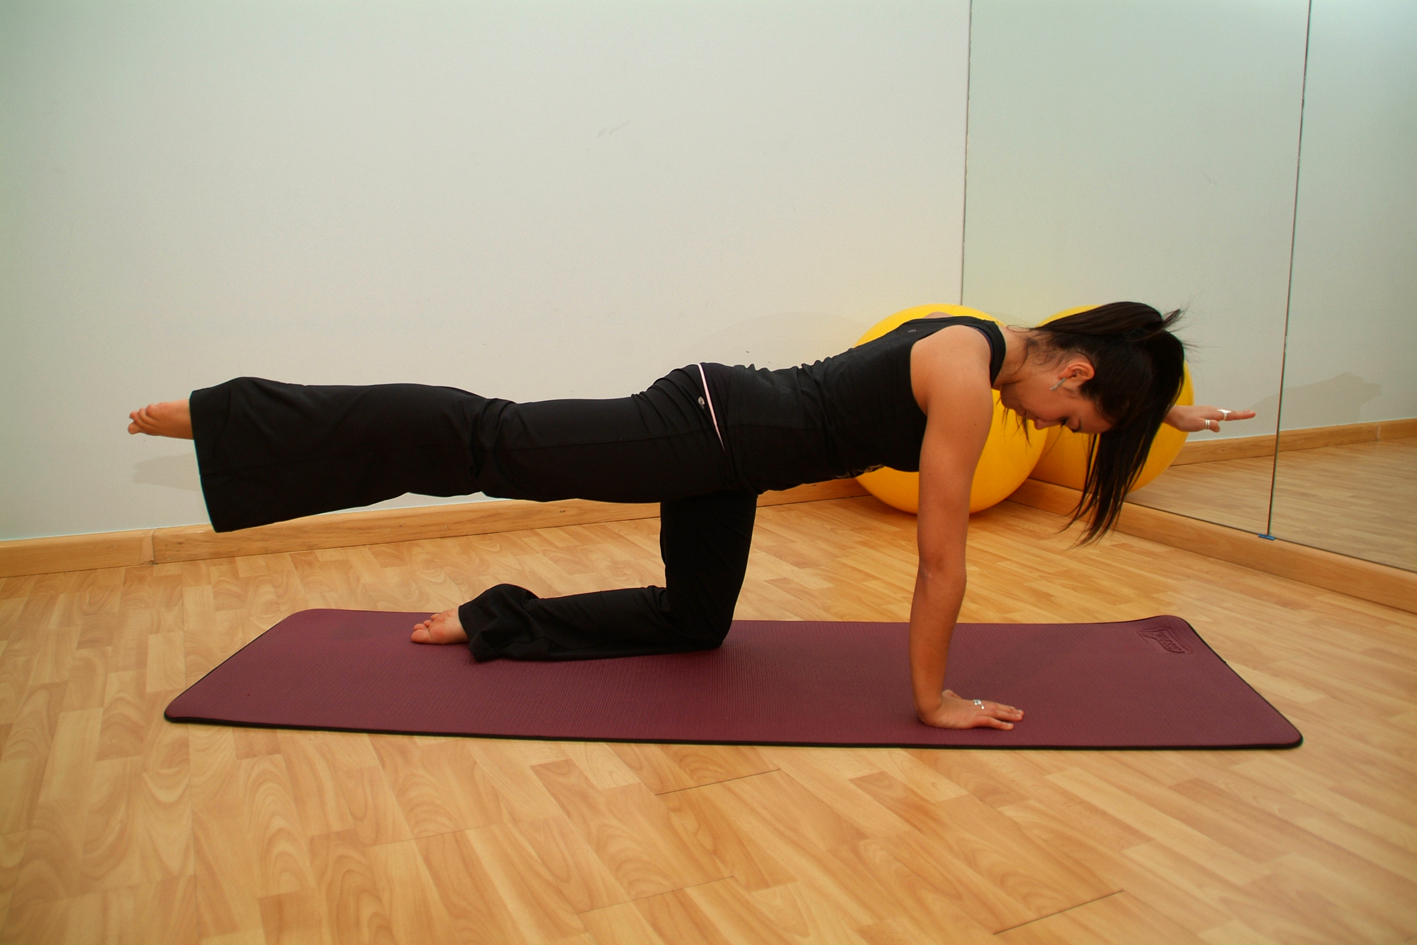
Floor spread for exercise

Floor finish systems classified by the method of laying or fixing are FOUR basic types.

  1.  simply laid on
  2.  mechanically keyed
  3.  adhesive bonded
  4.  cast in situ
1-SIMPLY LAID-ON FLOORING SYSTEMS

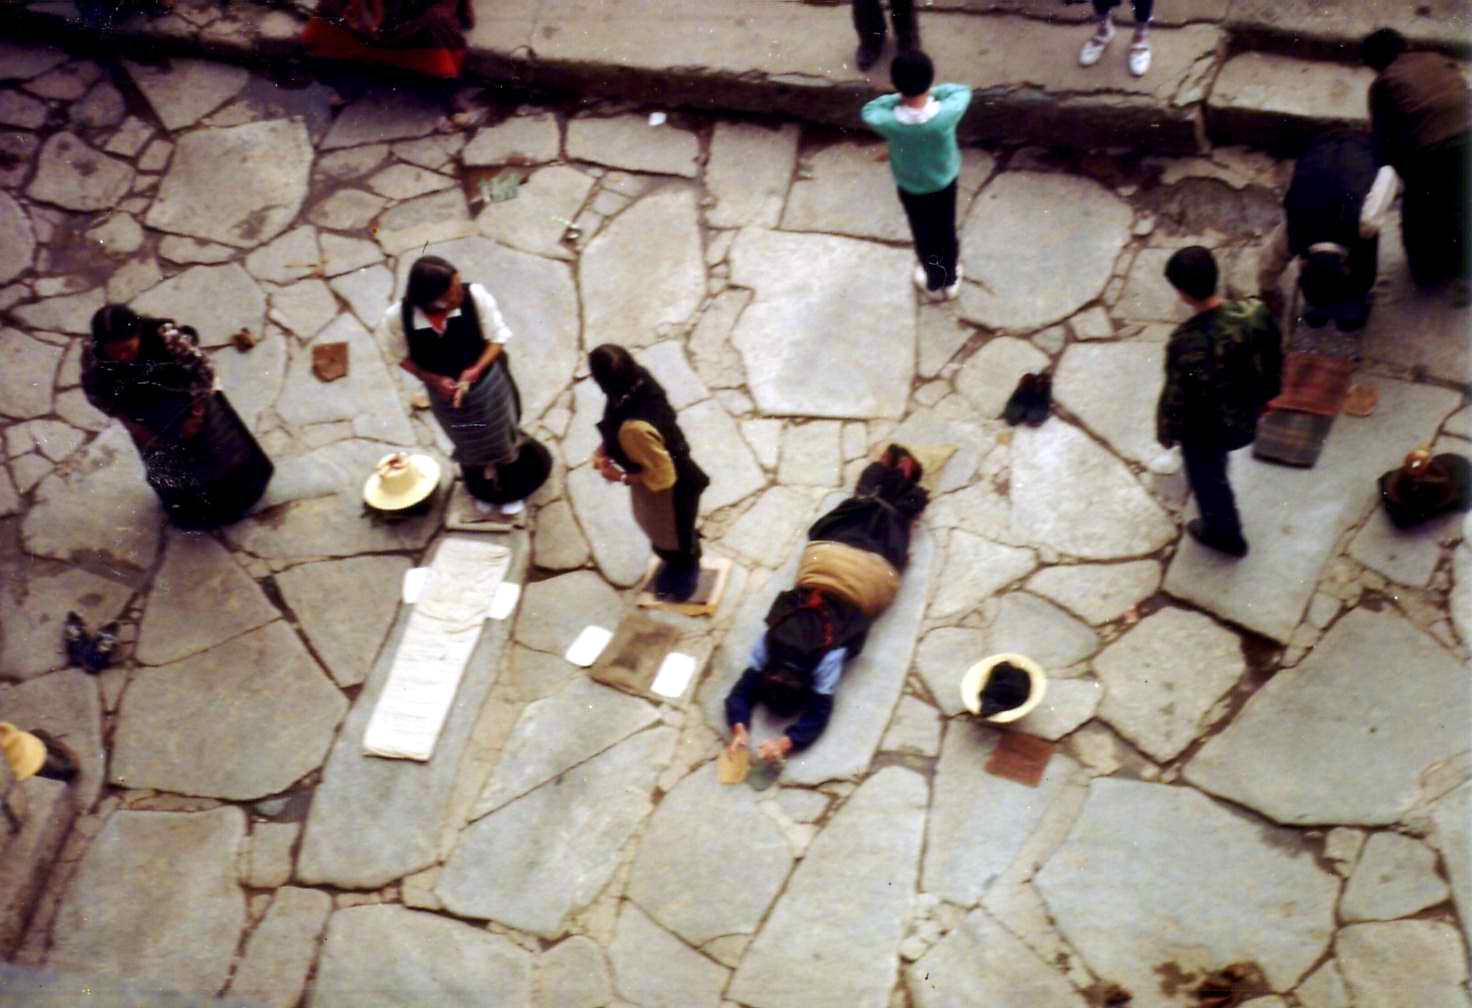
These flooring systems remain fixed due to the gravity. The materials are broad-based and often their sheer packing (tight conglomerations of several pieces) provides the stability. Such floorings do not work properly on inclined gradients and in vibratory conditions. Thin or low mass materials get blown off by winds, or get upset due to the moving traffic on it. These floorings are always demountable or removable, re-installable, so preferred for streets to facilitate alteration of service lines. These flooring systems are often secondary systems laid over a hard floor. Some gravity stayed floors are sparingly fixed or keyed by mechanical fixers (e.g. carpets by cleats, zippers, Velcro, etc.). In some instances backing materials like rubberized coating also improves staying by increased friction.

Large pieces of floor stayed by gravity

Cobble stone Floor


Examples: cobbles, brick lays, gravels, sand spreads, carpets, rugs, floor spreads, Daris, Chattais, woven mats, foot’s dusters, wooden boards, synthetic flooring mats, plastic and rubber tiles and rolls, lawn blocks.


2-MECHANICALLY KEYED FLOORING SYSTEMS

In this case the floor finish is incapable of staying in place due to thin body, low weight, absence of gravity pull (such as inclined, vertical or upside down surfaces), presence of other disturbing or vibratory forces, and small extent of spread. Such floors’ finishes are mechanically keyed to the substrate or the structure. Mechanical fastening is achieved by joining systems like nut-bolt, nails, screws, rivets, seam formation, stitching, etc. and also through: friction, suction, surface-tension, magnetic pull, electro-static attraction, etc.


Examples: bus metal floors, ship decks, stage wood floors, cladding, panelling, stair carpets, industrial and performance stage catwalks, etc.


3-ADHESIVE BONDED FLOOR SYSTEMS

In this system the Floor finish is stayed by affixing in Three distinct ways:

1 several small units of floor finish are affixed edge to edge to create a larger unit, so that it can due to sheer extent stay-put in a place,

2 the flooring material or a layered composition of it, are affixed to a base or substrate.

3 The floor finish is affixed to the substrate or structure, but a part of the fixing material is allowed to float up at the edge junction to form a joint.


Ceramic tiles fixing with cementing compound


Examples of adhesive bonded floors: Natural stones (Marble, Granite, Slate, Sand stone), Cast material (cement blocks, mosaic tiles, IPS, Ironite) synthetic tiles (PVC, linoleum, Glass fiber), Ceramic tiles (bricks, terracotta, baked clay, glazed, porcelain, highly vitrified) and films, foils.


4-CAST IN SITU FLOOR SYSTEMS

Cast in situ or site systems are laid on the site as a coating. The coatings are thin films, viscous mass or spread of substantial mass. These flooring systems provide a joint-less and uniform quality surface. The major advantage is that there are no visual or application joints, except formed due to fast setting or drying of applied material. The non existence of Structural joints creates one homogeneous surface. Such systems are usually designed to develop a bond with the substrate as the surface is formed by processes such as curing, evaporative drying, cooling, oxidation, calcification, chemical bonding, polymerization, heat, radiation and moisture induced changes. The bonding with the substrate reinforces it.

Concrete cast floor

Site cast flooring


Examples: concrete floors, Cement cast floors, cow dung, Surkhi and lime combinations, synthetic or culture marble systems, fiber glass and other resin+ fiber matrix spraying composites, Organo plastics, tar-bituminous materials, Paints (Enamels, Cyclized rubbers, Lacquers, Epoxies, Polyurethane, etc.).
.

Tuesday, February 10, 2015

BUILDING, USER and ENVIRONMENT

BUILDING, USER and ENVIRONMENT

Post 117 ⇒  by Gautam Shah ➔


Buildings, are more often designed to be inhabited by unspecified users. Many buildings in urban areas see increasing change of ownership. With every change in ownership the building is altered in various measures. The changes are extensive in older buildings surviving in upgraded or rejuvenated neighborhoods.

Style Buildings

Buildings conceived for style considerations are designed irrespective of their environmental settings. Such building’s have innumerable and excessive capacity systems to meet environmental anomalies. The systems are either irrelevant, or highly potent for many of the users.


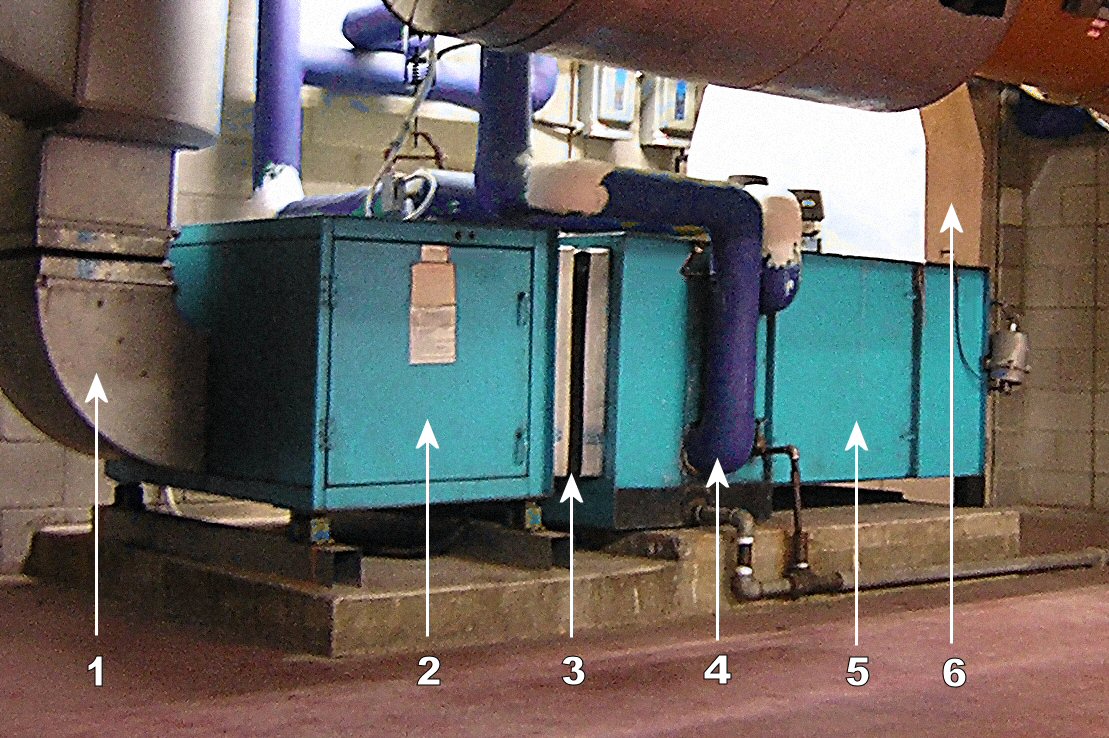
Air Handling unit

New owners of a building (or its section) have several choices to procure systems that are permanent, replaceable as a whole or partially up-gradable. The technological up-gradation of the building as a system occurs through replacement by an efficient system. There could be elimination of several sub systems by adoption of a comprehensive system. Integration of several systems by spatial rearrangement, rescheduling, segregated or comprehensive control. New owners, if aware would want greater use of passive systems instead of active systems, as it is long term economic relief and meets the environmental concerns. Reliance on sensing mechanisms, control elements, decision elements, connecting elements, distancing elements, converters, etc. leads to lesser chances of failure, quicker detection of problems, and faster replacement of failed system. New occupants have their own perception of safety and security, depending on their family profile and lifestyle. Similarly internal arrangements or space planning requirements must match the needs of the family, and this is an area of worry for the new occupant and also associated with every major change in the body of the family.


Left or Right orientation for Kitchen is one of th major causes of change > Flickr Image by


Changes in buildings are Intentional such as: functional, technological upgrading, styling. Changes are Circumstantial such as: due to ageing, wear and tear of use, overuse, under-use, non use, and misuse. Environmental changes are adoptive ones, where the new user customizes the building by self-help, but changing only the familiar and easily removable subsystems, etc. For altering partially integrated or coordinated subsystems, one needs the services of crafts-persons or specialists. 

Security Devices
.


Sunday, January 25, 2015

PLASTICS FINISHING

PLASTICS FINISHING
Post 116 ⇒  by Gautam Shah ➔
.

The basic purpose of finishing plastics is to remove the nominal imperfections such as scratches, dull spots, dents, protrusions, ridge marks at the junction of moulds, gate marks (entry points of pour). Many of these are avoidable by refined production methods. For finishing, primary techniques like grinding, filing, sanding, buffing, turning, tapping, sawing, etc. are used. Most post-production finishing processes are required for preparing or readying the item for subsequent manufacturing. These are, drilling, splitting, chopping, trimming, cutting, grinding, etc. Plastic products like granules, fibres, powders, liquids, etc. Go through several cycles of finishing and further manufacturing before a utilizable product is achieved. Some plastic entities need a micro size calibration to meet the tolerances’ requirements.

Mechanically ground edges

MACHINING

Rigid plastics, thermoplastics and thermosets can be machined by conventional processes such as drilling, sawing, turning on a lathe, sanding, and other operations. Glass-reinforced thermosets are machined into components like gears, pulleys, sprockets and other shapes, when the small batch size cannot justify fabrication of moulds. Various forms can be stamped out (die-cut) from sheets of plastics. The cups made by vacuum forming, for instance, are cut out of the mother sheet using a sharp die. In the case of a thermoplastic such as polystyrene, the scrap sheet left over, can be re-ground and re moulded. Soft thermoplastics need proper support to prevent distortion during machining. The elastic recovery in plastic materials with low softening point requires precautions so that shrinkage and distortions are prevented, such as with tapped holes that become tapered or smaller than the nominal requirements. Plastics show heat-build up during machining which causes gumming, discolouration, poor tolerance control.

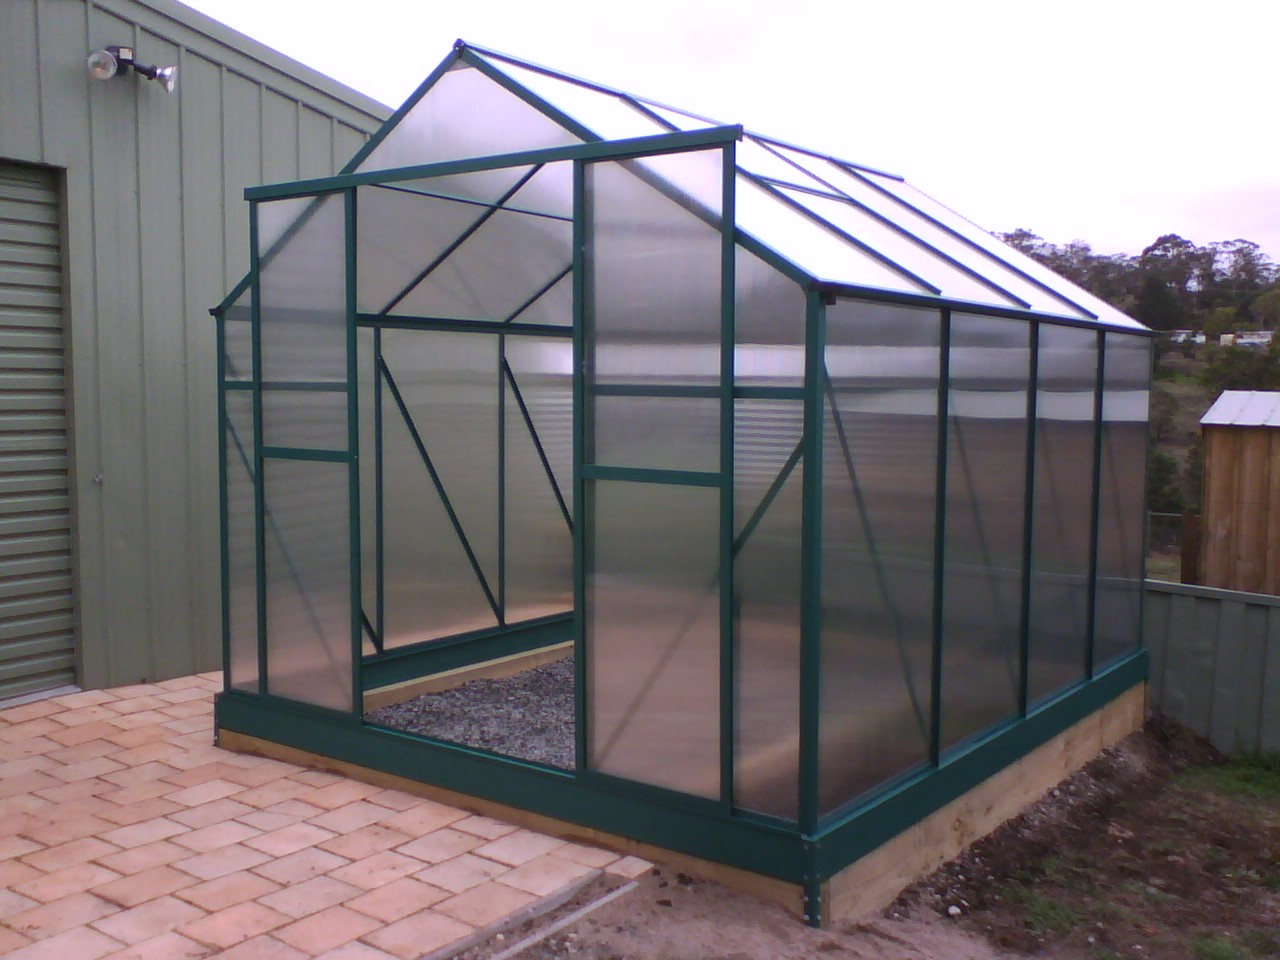
Treated surface Polycarbonate Greenhouse

DRILLING, TAPPING, THREADING, RAMMING

These operations relate to speed, which in case of thermoplastic depends on the type of material, size and depth of the hole. Speeds that are normal for harder materials must be reduced for softer materials and larger size of apertures so as to minimize the heat generation. Thermoplastics require, slightly oversized hole to offset the shrinkage due to elastic recovery of material.

SAWING

Reinforced thermosetting plastics and dense thermoset usually give clean saw-cut. Thermoplastic materials with low melting temperature become soft due heat of friction during cutting. Deep sawing becomes difficult as the saw gets jammed due to elastic recovery of side walls.

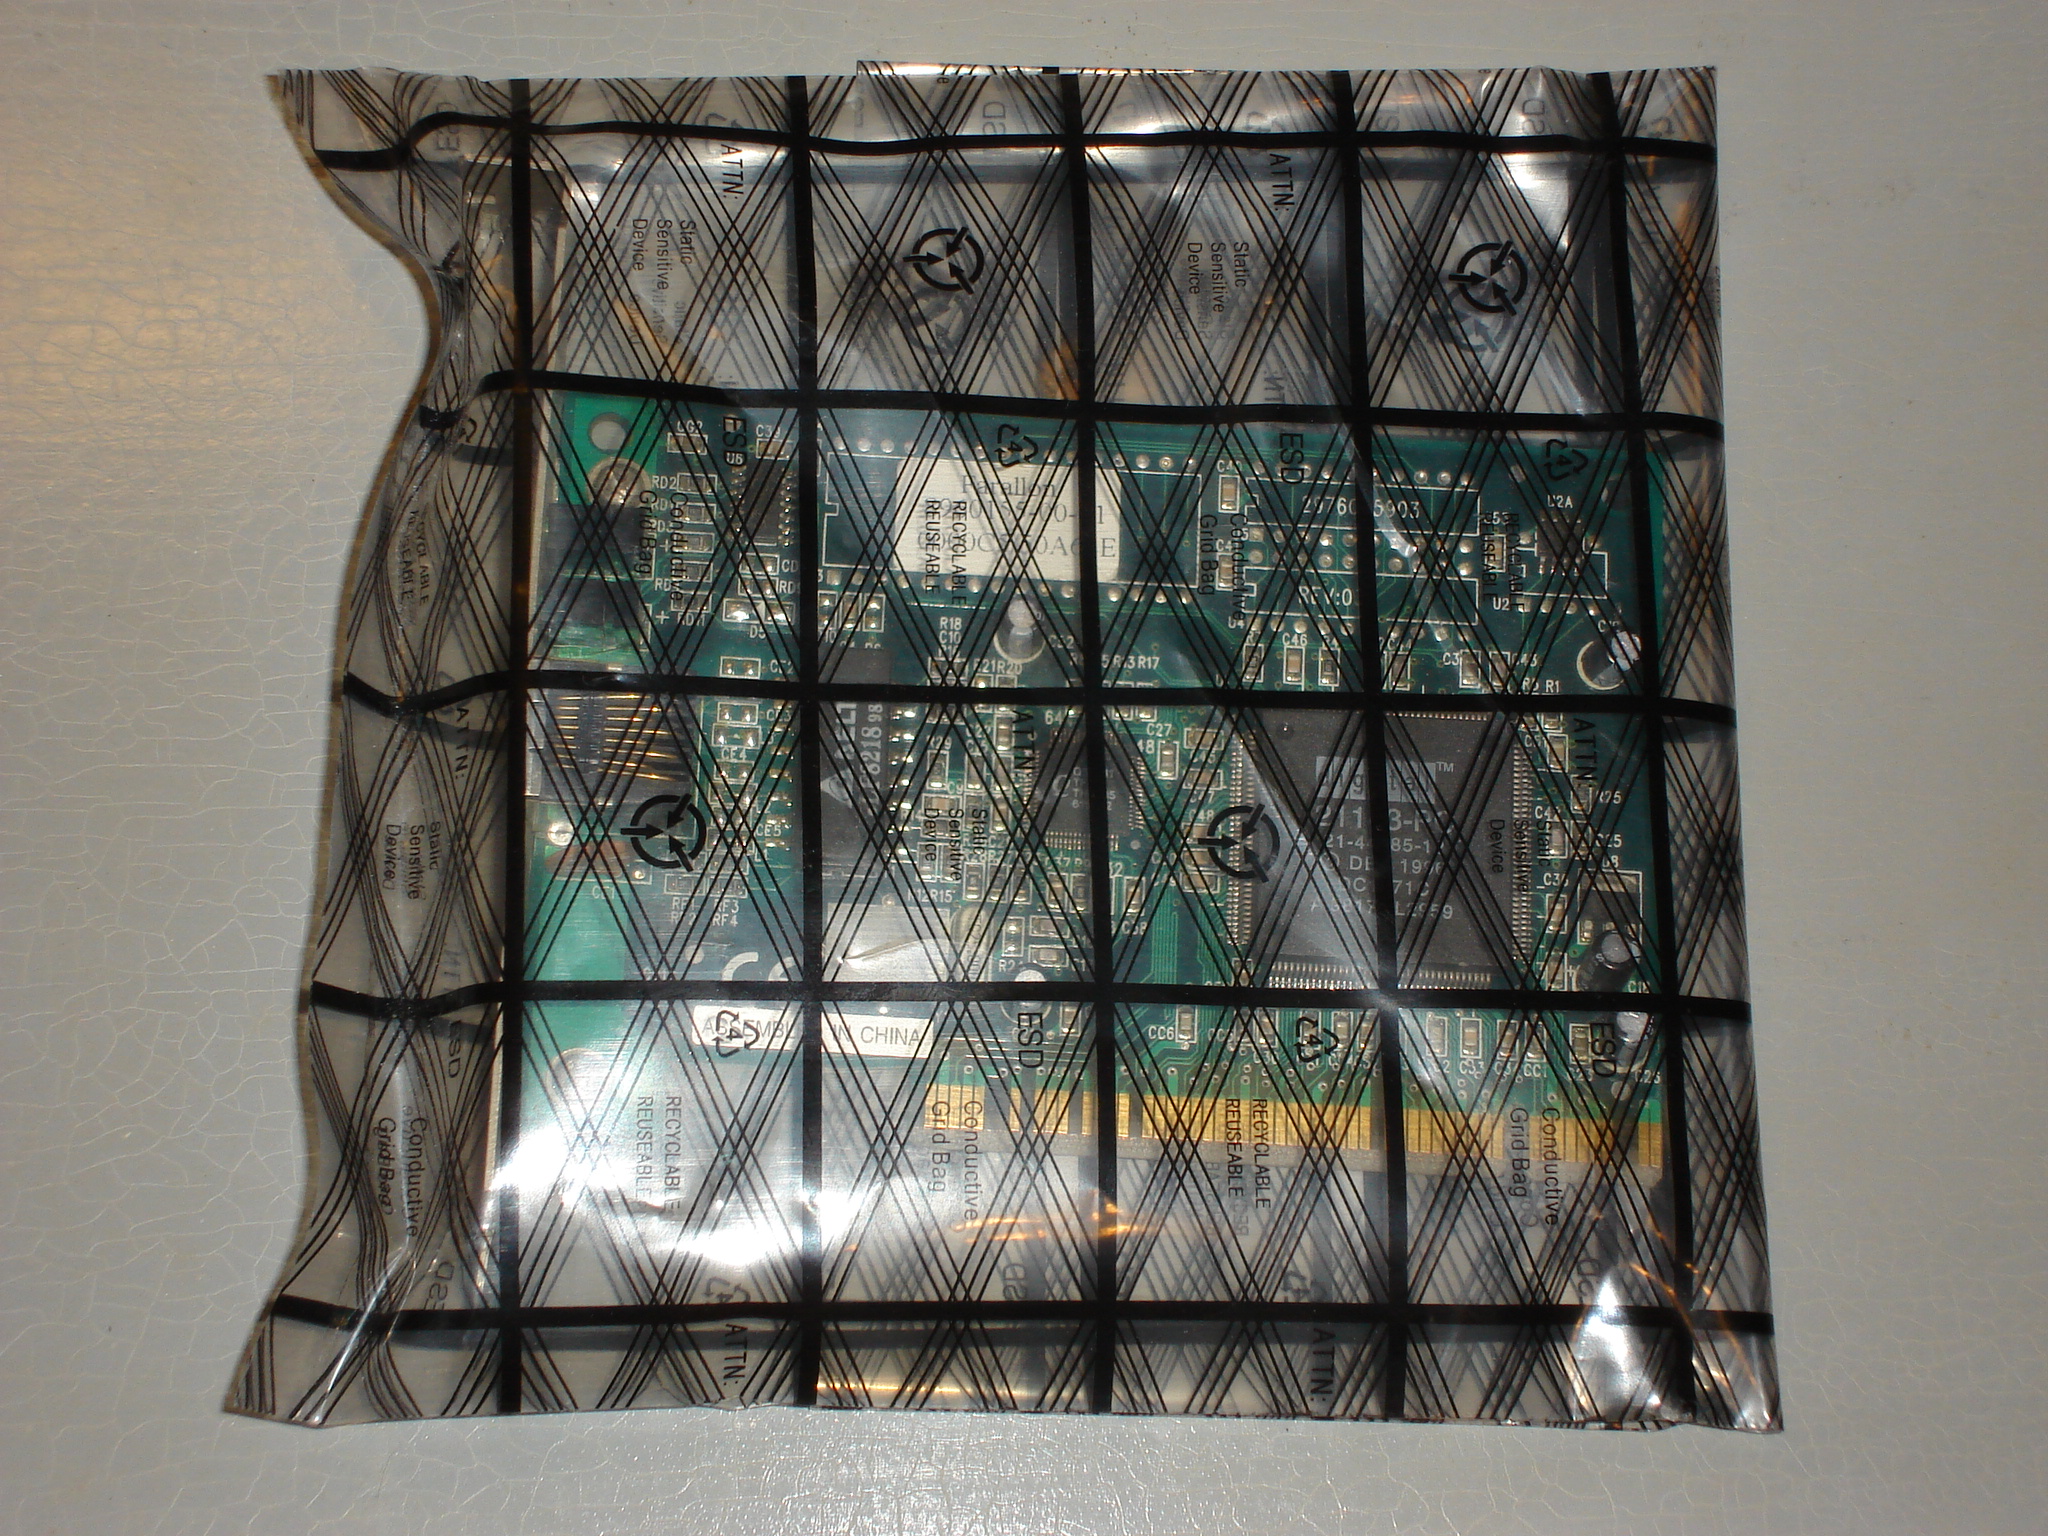
Anti-static bag for packing electronic items 

DECORATING PLASTICS

Plastic articles are decorated for technical, functional and sensorial purposes. Colour coats reduce the penetration of UV rays from sun light, whereas clear coats are used for toys and edible storage utilities. Colours are included by multi point injection moulding, or by mixing polymers with slightly a different melting point. Plastics are coloured by paints and organo-sol (liquid plastic formulation) through brushing, spotting, dipping and spraying. For texturizing and branding pad printing, hot-stamping, silk screen printing, are used. Screen printing is done for flat and round surfaces such as dials, bottles etc. Hot stamping and heat transfers involve transferring a pre prepared design from a soft flexible film or foil with heat and pressure. Other than this there are many types printing processes that transfer an image or patterns to specific areas of plastic objects. These include flexography, offset, etc. Valley printing deposits colour only in the depressions. Roller printing deposits colour on the level or ridge like surfaces. Toys and household articles are decorated by a variety of temporary and permanent stickers (labels) that are usually overprinted but in transparent stickers these are under printed. Preprinted designs on foil or film of a compatible material can be inserted in the mould before injection of thermoplastic material.


Embossed Plastic film


Plastic articles are hot and cold stamped by heated plates, rollers, etc. that are engraved or etched with designs, patterns, logos, etc. Rexine, wall papers have such patterns. Plastic surfaces are machine or laser engraved to create patterns or texture. Amorphous plastics such as Acrylics and poly-carbonates are engraved. Acrylic plastics are finished with flame polishing. Extruded plastics are provided with Corona treatment, referred to as air plasma, to modify the surface qualities.


Polished Poly(methyl meth-acrylate)

Many plastics are sensitive to solvents so latex dispersion paints, NC clear and pigmented Lacquers, epoxies, etc. are applied. Plastics need to have electrically conductive surface which is imparted through plating and vacuum metallizing. It can be made to certain categories of plastics such as ABS, Polypropylene, Polyesters and some Nylons. Electroplating is done to achieve matt or glossy surfaces. Automobile accessories, tape, radio and TV trims have electroplating finish for providing metal like a look. Metals in very fine particulate size are deposited on plastics not only to provide metal like a look but also provide electrically a conductive surface. Vacuum metallizing involves spraying vaporised metal on a plastic article in a vacuum chamber (to prevent oxidation). Electrical parts, auto-spares, toys, artificial Jari threads, sun control films, etc. are, metallized in a variety of silvery, golden, copper or bronze effects using aluminium compounds. Gold, Silver Palladium, Platinum Coppers etc. are applied through a cathode (electrodes) sputtering. Metals are also spray deposited through suspensions.

Indian Space Satellite wrapped for Protection in Polyester Gold metallized foil 


.

BERNARDO BELLOTTO

  BERNARDO BELLOTTO Post -376 SUNDAY Feature on ART of Architecture -by Gautam Shah BERNARDO BELLOTTO (1720-1780) was born in Venice (d...